
Blog
Discover our latest articles and blogs
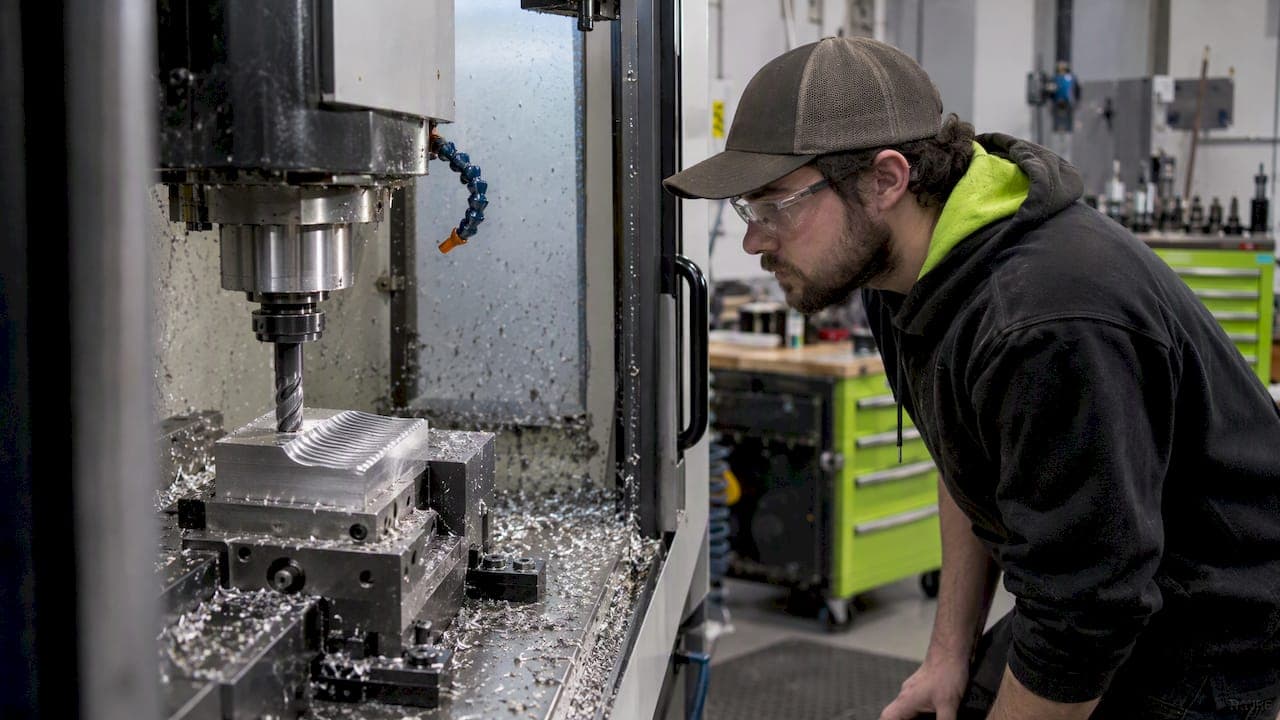
Stop Milling Chatter Without Sensors: 4 Shop Fixes for Prototype Work
Shop-tested methods to stop milling chatter on prototype and short run jobs. Four quick, low cost fixes quiet most chatter before sensors or modal testing.
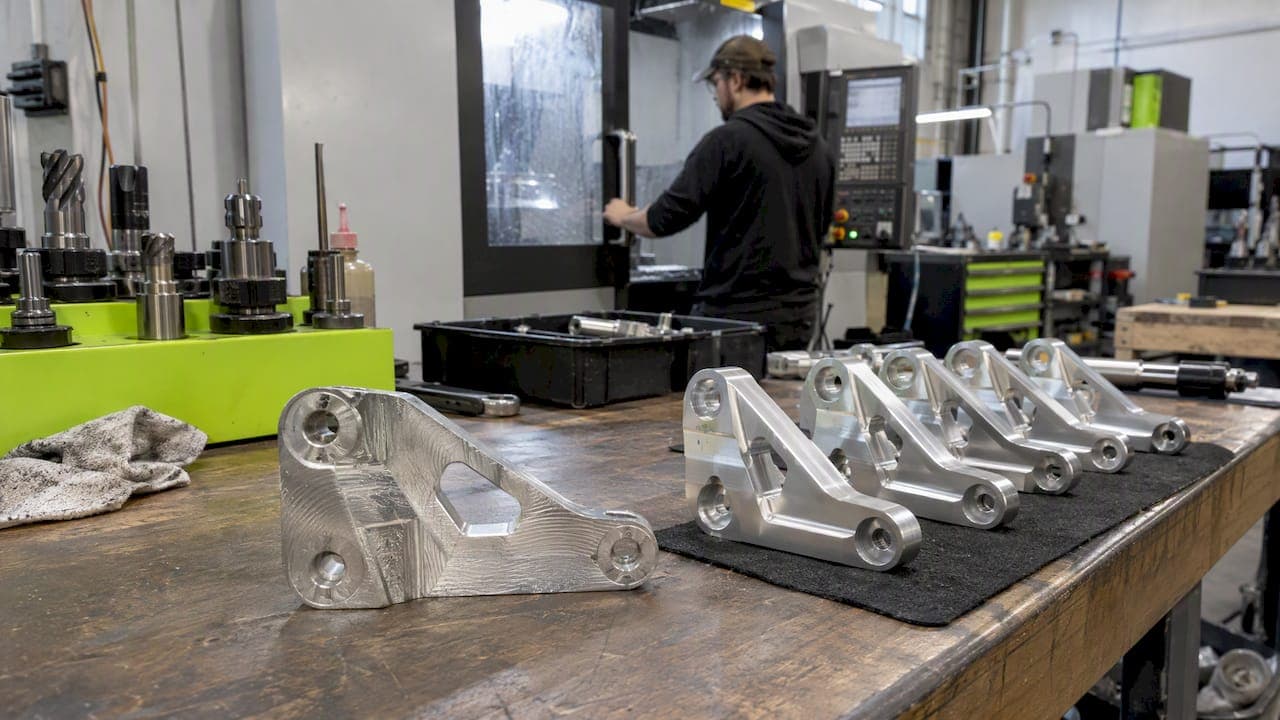
2 to 3 Day Prototypes: Prototype to Production for Motorcycle Parts
Shop-focused steps to move a CNC prototype into repeatable short run motorcycle and mechanical parts. Covers GD&T, FEA, fixturing, and first-article...
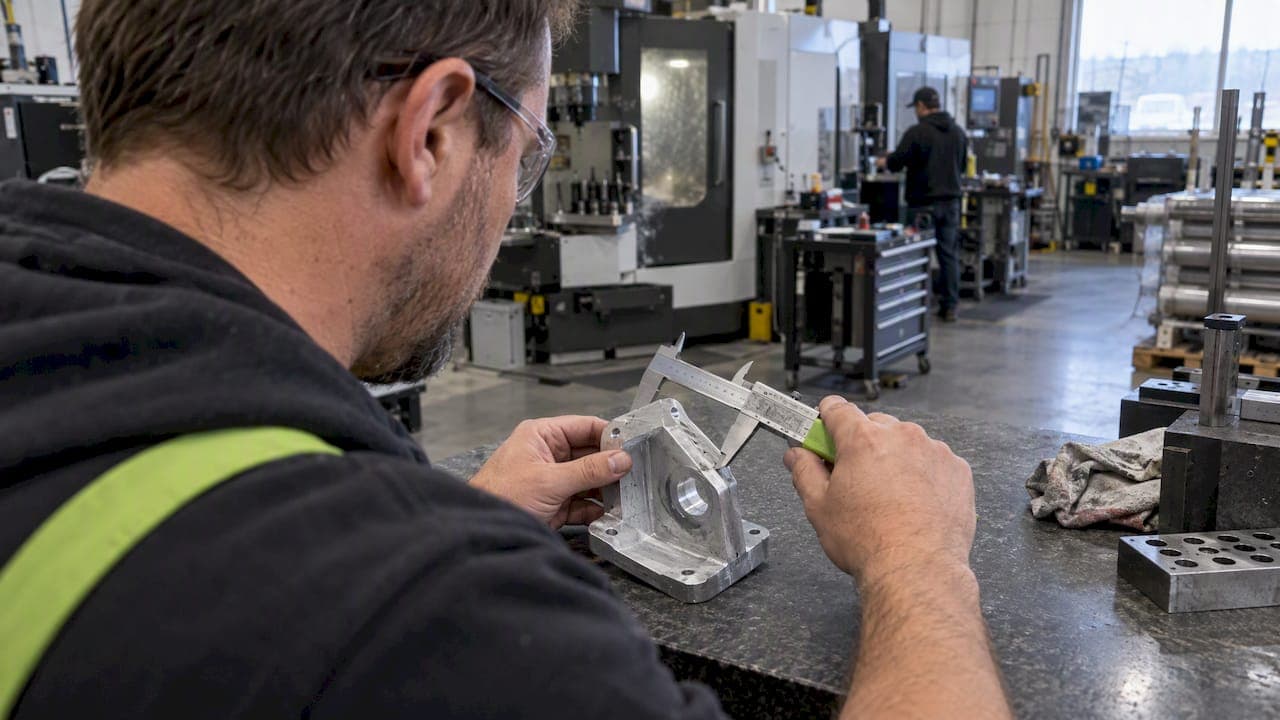
Rebuild Intent & Fit: Reverse Engineering Without Drawings for Shops
Shop ready scan to CAD workflow for reverse engineering without drawings. Reconstruct intent, set tolerances, verify parts for production.
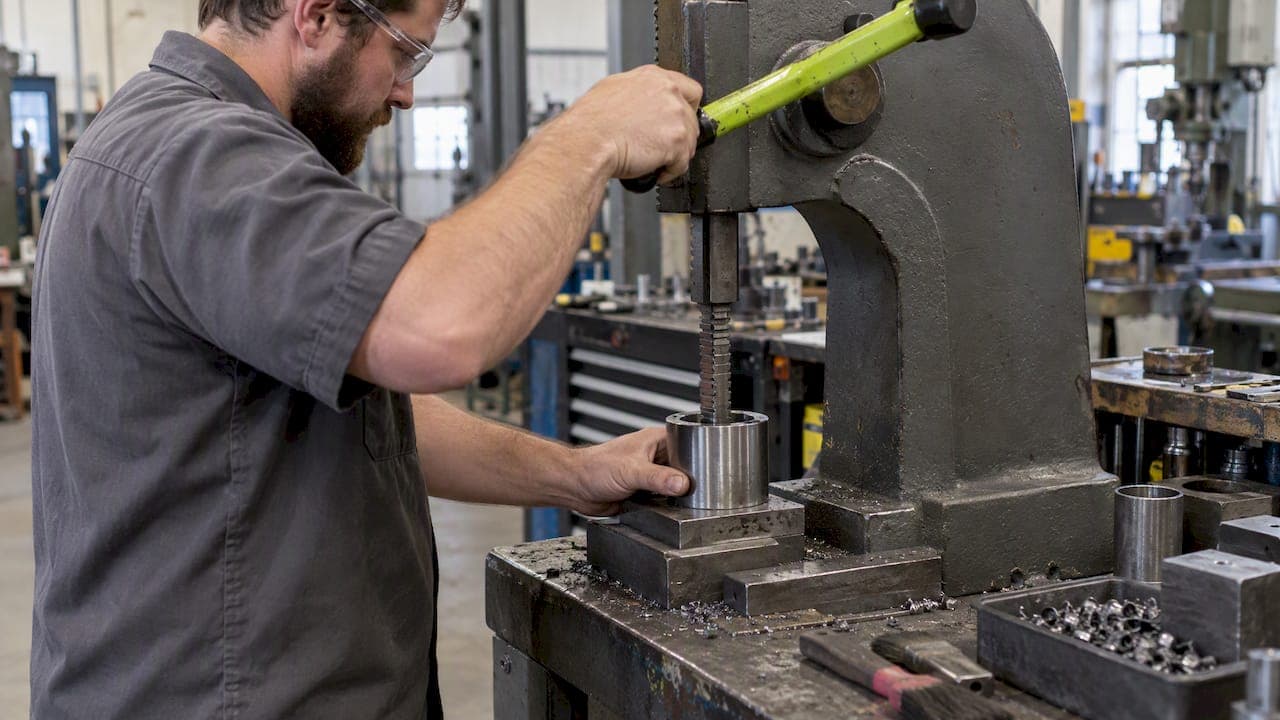
Stop Scrapping Parts: Shop First Keyway Broaching Rules for Machinists
Shop ready keyway broaching workflows, fixture and bushing checks, machine options, and troubleshooting for machinists. When to choose push, pull, rotary,...
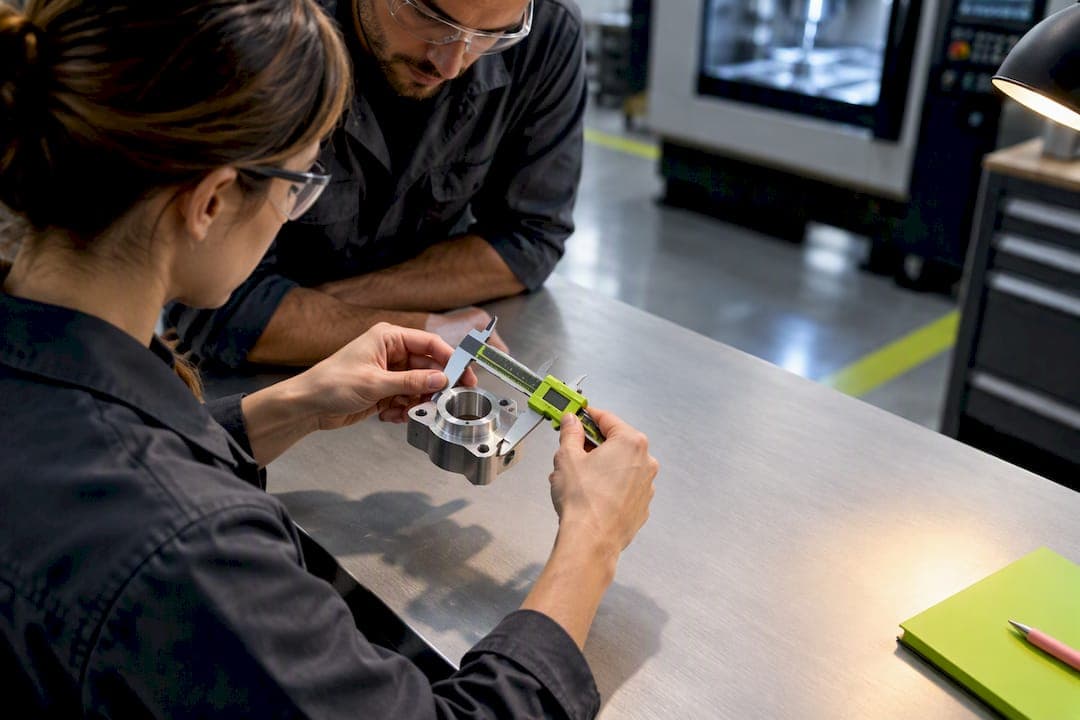
12 Machine Shop Questions Engineers Must Ask Before Quoting
A prioritized 12-question checklist to vet a machine shop: verify GD&T (ASME Y14.5), CMM reports, outsourced-process controls, quoted line items, and...
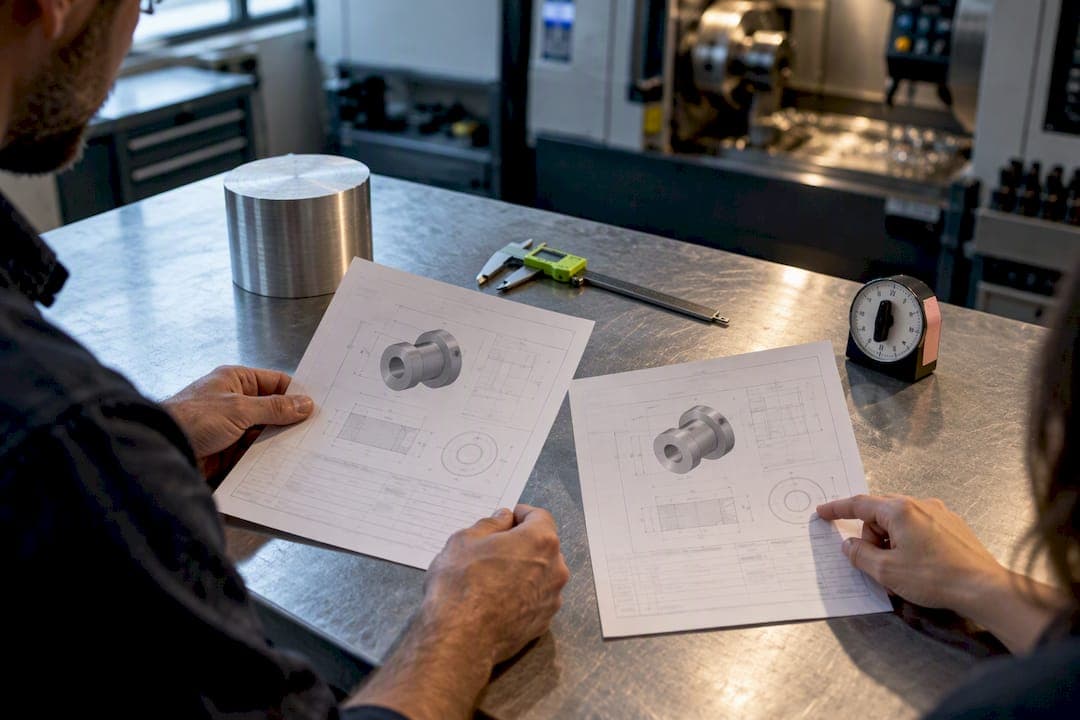
Sanity Check CNC Prototyping Cost: Shop Checklist for Small Businesses
See what drives CNC prototyping costs, use a shop proven checklist, and run a worked $100 one off example to sanity check any quote.
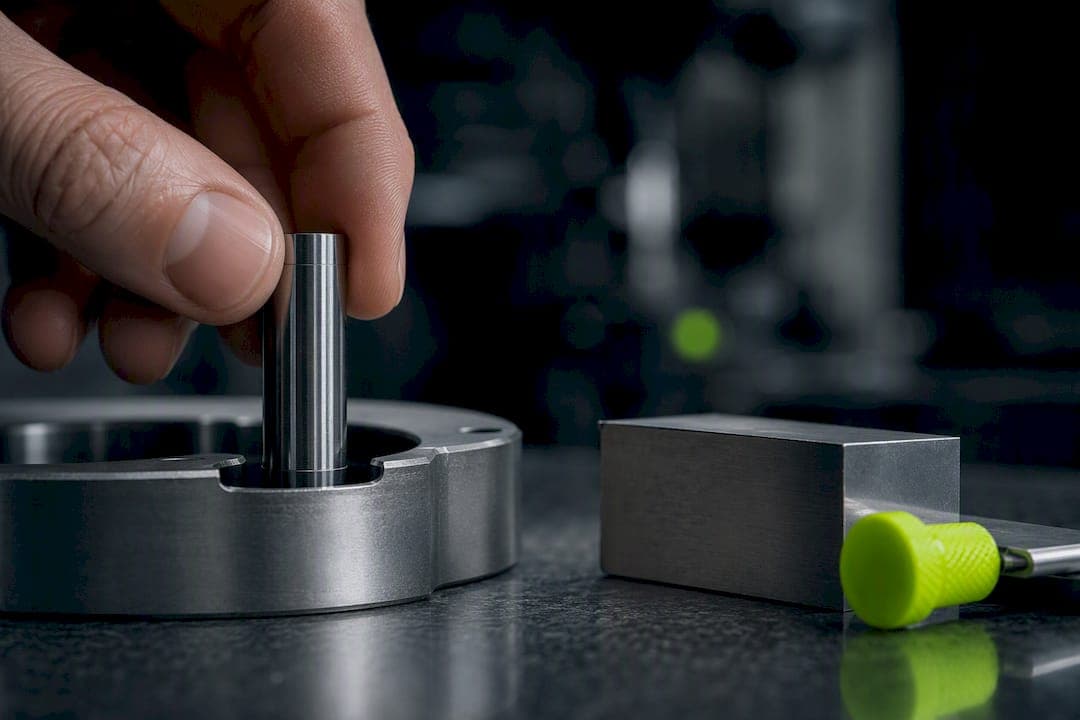
0.0005–0.005 in Slip Fit Tolerances: Spec Ready for Engineers
Compact, spec-ready reference of slip-fit clearances (0.0005–0.005 in) with sourced charts, shop-tested machining steps, and verification tips engineers...
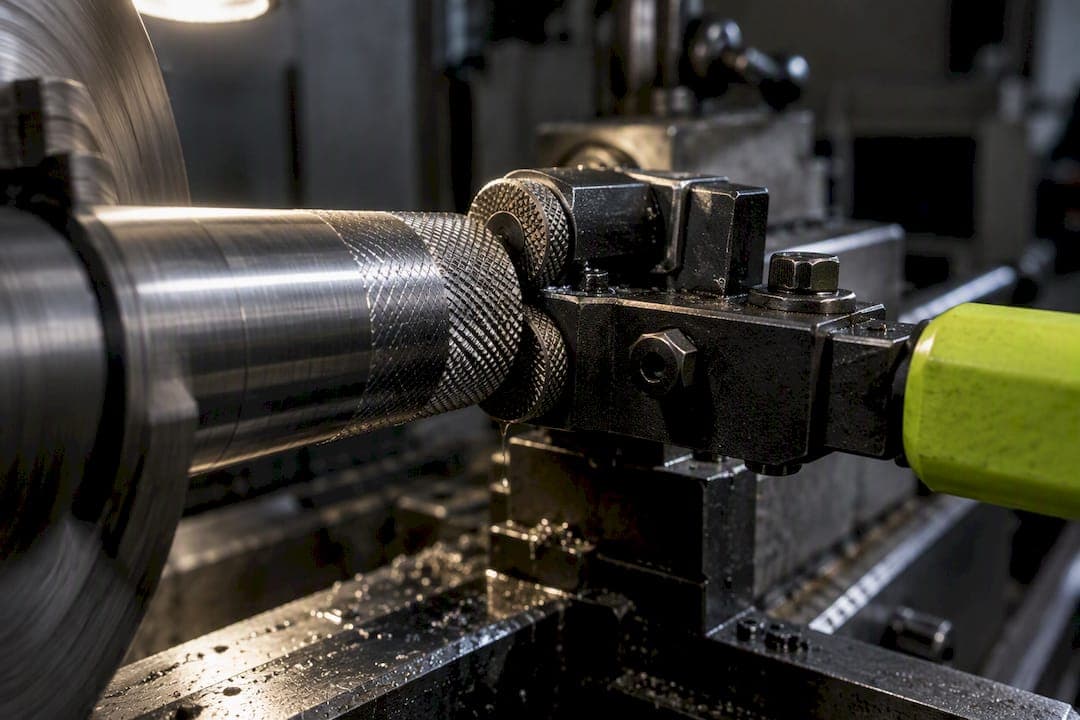
3 Knurling Types That Define Grip, DIN Codes, Form vs Cut, 300 RPM
Master the three knurling types: straight, diagonal, diamond. Use DIN codes, choose form or cut, and follow a 300 RPM baseline for prototype and short run...
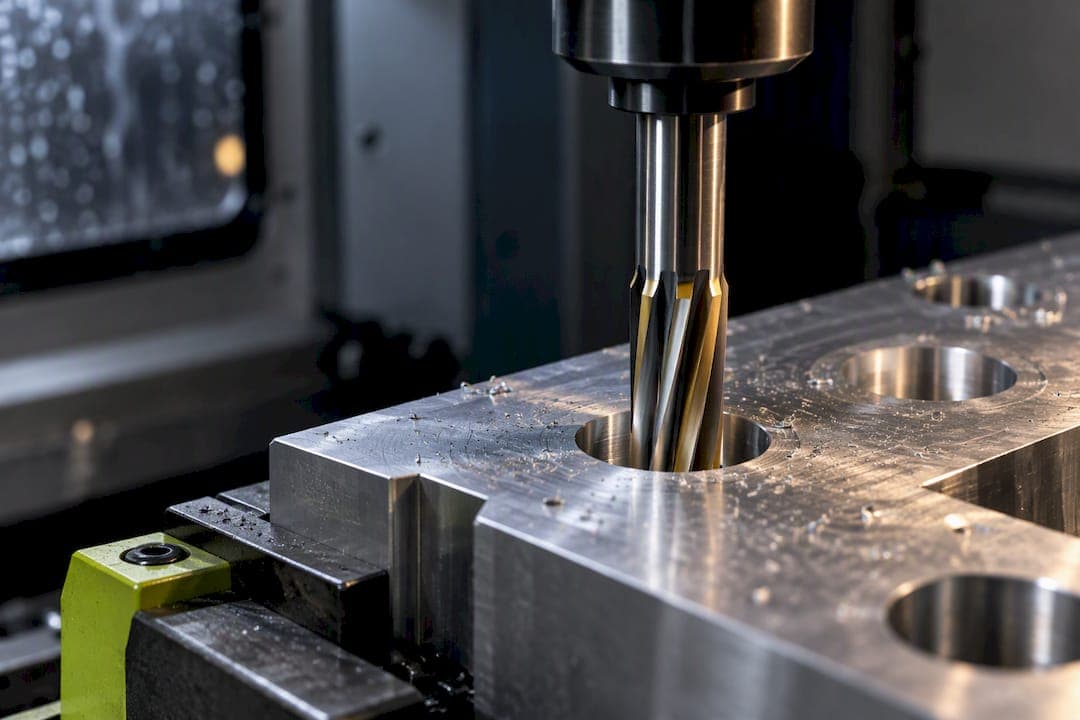
Leave 0.007 in Before Reaming: Shop Rules for Reaming vs Drilling
Shop-proven rules for when to drill or ream: reaming removes about 2–5% of the diameter. Leave 0.007 in on steel and 0.012 in on aluminum to avoid chatter...