
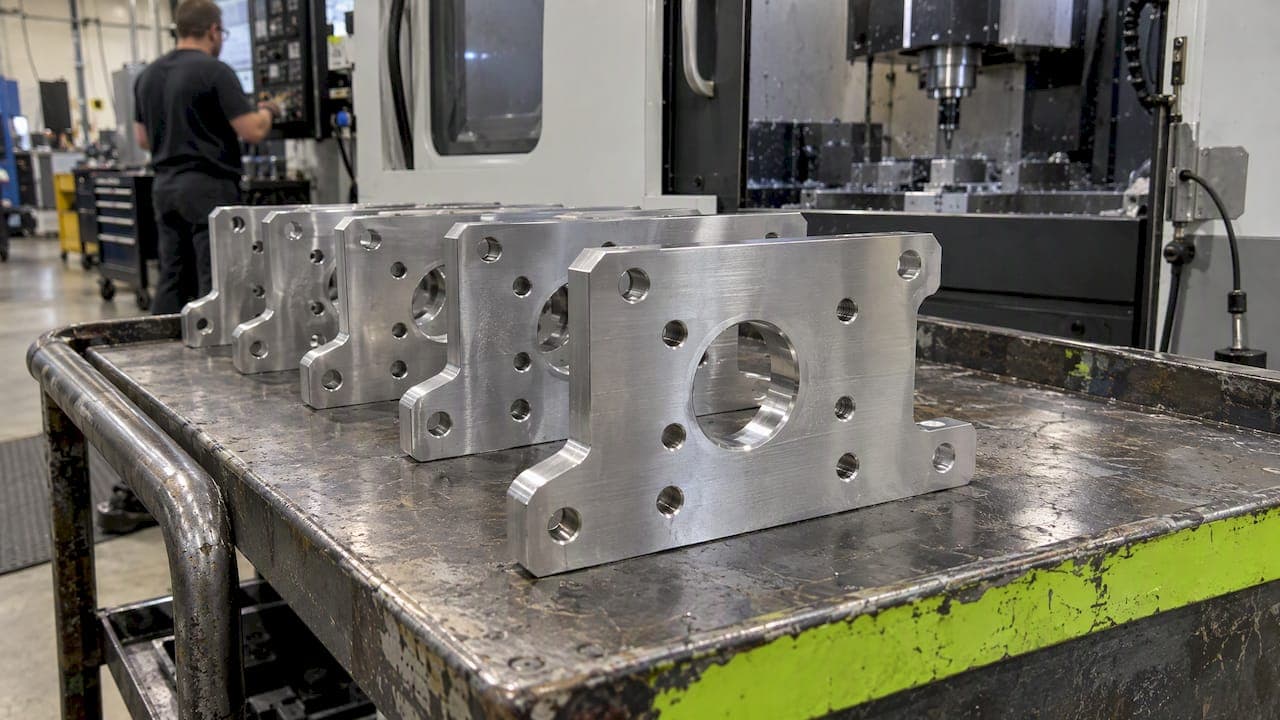
Repeatability in machining is a machine's ability to do the same thing again and land in the same place, cycle after cycle. It says nothing about whether that place is the right one. That second question is accuracy. A machine can be tightly repeatable and still cut every part 0.002 in. too big. A shop that understands the difference can fix the offset in minutes. A shop that confuses the two chases scrap for days.
This guide covers what the term means, how it differs from accuracy and reproducibility, how it is tested, and what actually keeps it stable on a real job. We machine prototypes, short runs and motorcycle parts in Athens, Alabama, so the examples come from that kind of work.
TL;DR
- Repeatability is how closely the same motion or result is duplicated. Accuracy is how close the result is to the commanded or true value. You need both, and they are fixed in different ways.
- A builder's repeatability figure is a static axis test. Finished-part consistency also depends on fixturing, tooling, heat, chips and inspection.
- Reproducibility is a different claim: same result across machines, operators, fixtures or days.
- For short runs, ask how a capability was tested, then verify with a tool-setting check, a warm-up routine and a few measured parts.
Repeatability vs. accuracy: the plain-language difference
Think of a drill hole pattern. Ten holes in a tight cluster, 0.01 in. off the target, is repeatable but not accurate. Ten holes scattered around the target, averaging right on it, is accurate on average but not repeatable. The goal is a tight cluster on the target.
Modern Machine Shop's Mike Lynch frames it for CNC specifically: accuracy is how precisely the axes follow intended paths to commanded endpoints under load, and repeatability is how precisely they duplicate commanded motions, again under load. The "under load" part matters, and we come back to it below.
Here is why the split is useful in practice:
| Repeatability | Accuracy | |
|---|---|---|
| Question it answers | Does it do the same thing every time? | Is that thing the correct thing? |
| Type of error | Random scatter | Systematic offset |
| Typical fix | Better workholding, thermal control, tool and spindle condition, process discipline | Offset, calibration, compensation |
| Shows up as | Part-to-part variation | Every part wrong by a similar amount |
A systematic offset can usually be dialed out. Random scatter cannot be offset away. That is why a repeatable but slightly off process is often easier to fix than an inconsistent one. A peer-reviewed review of traceable on-machine measurement makes the same point: machine repeatability and temperature variation are major contributors to uncertainty, and systematic errors may be compensated, but random repeatability errors must be measured, controlled and included in the uncertainty budget.
Repeatability vs. reproducibility
The two words get swapped constantly, and in a quote or a quality plan the swap causes trouble.
In metrology, repeatability holds the operator, equipment, method, location and short time interval substantially constant. Reproducibility changes one or more of those conditions. The NCBI Bookshelf's metrology box lays out that scale of conditions, including the in-between idea of intermediate precision, such as different days in the same lab.
In a machine shop that translates into two separate claims:
- Repeatability: this machine, with this fixture and this program, makes part 1 and part 50 the same.
- Reproducibility: the same part comes out the same on a different machine, with a different operator, a different fixture, or next month.
A prototype customer who later moves to production cares about the second claim far more than the first. If you plan to scale a design, ask how a shop proves it holds across setups. Our post on gage R&R for CNC shops shows how three operators and ten parts expose measurement variation that people assume is machining variation.
What the standard actually measures
The reference most buyers hear about is ISO 230-2. The standard covers the determination of accuracy and repeatability of positioning of numerically controlled axes. It applies to linear and rotary axes and is used for type testing, acceptance testing, comparison testing, periodic verification and compensation. It requires repeated measurements at each position, with associated uncertainty estimates.
Two limits are worth keeping in mind:
- It evaluates axis positioning. It does not guarantee the dimensions of every finished part.
- It is a test of the machine under defined conditions. Your part has a material, a cutter, a fixture and a cycle time that the test did not include.
So when a machine's brochure lists a repeatability number, treat it as a useful starting point. It tells you the axes are capable. It does not tell you what happens at hour six of a production run cutting 6061 with a long end mill.
Why the spec sheet is not the finished part
NIST describes precision machining as the ability to repeatedly manufacture parts to specified tolerances. Those tolerances can govern size, form, surface finish and relative location. Axis repeatability is one input into that larger system, alongside geometry, surface integrity, machine errors, measurement and compensation.
The static-versus-dynamic gap is where most surprises live. Practitioners distinguish a builder's static specification from in-process repeatability. Cutting forces, changing loads, warm-up, workholding, tooling and chip contamination can make a machine repeat differently during a job than it did in an unloaded acceptance test, as the Modern Machine Shop article explains.
Tool-point dynamics matter too. NIST's milling stability study shows that stability varies with operating conditions, so a cutting condition chosen from a single measurement can later land in an unstable region. For short-run work, that means validating under representative fixturing, tool wear, speed, feed and engagement, not just on a warm, empty machine.

The six things that move repeatability on a real job
1. Heat
Thermal growth is the quiet one. NIST's June 2026 research reports that thermal deformation from motors, machining and ambient temperature change can dominate volumetric machine error. Their measurement-and-compensation process took under 100 seconds and cut errors by up to an order of magnitude on the test artifacts. That was demonstrated on specific specimens, so any shop has to validate it on its own machine. An earlier NIST paper describes a vision-based method for monitoring thermal drift using a wireless microscope in the tool holder.
You do not need a research lab to act on this. A consistent warm-up routine, a stable shop temperature and a habit of checking a known feature mid-run are practical controls.
2. Workholding and datum strategy
If the part sits in a slightly different place each time, the machine's axis repeatability is irrelevant. Hard stops, dowel locations and a fixture that references the same surfaces every load do more for repeatability than most machine upgrades. Our dowel pin hole tolerance reference covers how to specify those locating features so a fixture goes back together the same way.

3. Tool setting
A wrong tool length offset looks like a machine problem and is really a setup problem. NIST's on-machine measurement guidance gives a simple check: measure tool length 10 times using the manufacturer's cycle with the spindle stopped, and calculate the range. The same document links automated measurement to fewer manual offset-entry errors, less rework and scrap, and better repeatability than manual cut-and-measure methods.
4. Probing
Probing is not a free pass. NIST reports that common machine-tool probes typically have repeatability of 1 micrometer or less, though full uncertainty depends on the machine and application. In a separate NIST evaluation of on-machine probing, simulated probing errors were 1.4 and 1.7 micrometers for 2D and 3D, and machine positioning error contributed as much as 44% of probing error in the tested scenarios. Those are results for one probe system, not universal values. The lesson: a probe's nominal spec cannot establish finished-part accuracy. We walk through the routine in 4 calibration steps for on-machine probing.
5. Tool wear and chips
A cutter that is slowly wearing makes size drift in one direction. Chips packed in a pocket or on a locating surface shift the part. Both are process controls, not machine capabilities: scheduled tool changes, air blast or flood before every load, and a quick wipe of the datum faces.
6. Measurement itself
If your gage cannot resolve the variation you are chasing, you will see noise and blame the mill. Measurement uncertainty needs to be well below the tolerance. For more on this, see our guide to tight tolerance machining for engineers.
Worked example: a 25-part bracket run
Suppose a drawing calls for a bore at 0.500 in. with a tolerance of +0.001/-0.000 in. across 25 brackets. Here is how a repeatability-minded shop approaches it. The numbers are illustrative, not a client case.
- Warm the machine with a standard routine before the first cut, so the first part and the twenty-fifth see similar thermal conditions.
- Check tool setting: run the 10-measurement range check on the finishing tool. If the range is a meaningful slice of the 0.001 in. band, fix the tool setter before cutting.
- Cut a first article and measure it on a gage with resolution well below the band.
- Apply one offset if the bore is consistently off in one direction. That is accuracy: a systematic shift.
- Run parts 2 to 5 and measure again. If the numbers tighten around the target, repeatability is fine. If they scatter, look at fixturing, chips and heat before touching the offset again.
- Sample through the run, for example every fifth part, and record the results. Our post on SPC for prototype machining shows how to catch drift before part 200.
Notice that step 4 and step 5 are separate decisions. Treating scatter as an offset problem makes parts worse, because you keep chasing noise.
What to ask a shop before you place a job
You can learn a lot in a five-minute conversation. Good questions:
- How was the machine's quoted capability tested, and does that test resemble my material, tool engagement and cycle time? That is the practical implication of Lynch's point about testing under load and across the day.
- What is the first-article and in-process inspection plan for my quantity?
- How are parts located in the fixture, and is the fixture dedicated or modular?
- Are tolerances on my drawing realistic for the feature? A tight axis figure is not enough if the drawing tolerance and inspection method do not fit together.
- Who actually runs the job? If the person quoting is not the person machining, details get lost between them.
That last question is one reason we run the shop the way we do (more below). For customers heading toward formal approval, our Level 3 PPAP walkthrough for machining shops shows what documented repeatability evidence looks like. Callouts matter as well: the true position basics and perpendicularity callouts posts cover how to write them so inspection and machining agree.
Our perspective: repeatability is a habit, not a number
We design, machine and ship everything from one shop in Athens, Alabama, and the person who answers your question is the machinist who builds the part. That shapes how we think about repeatability.
We make our own product, the E2 Kickstand for the KTM SX-E 2, GASGAS MC-E 2 and Husqvarna EE 2. A kickstand has to fit a specific mounting point on every bike, the same way, for every parent or rider who orders one. If the hole pattern or the stand geometry wandered from one batch to the next, someone would find out in their garage. Making our own parts keeps us honest about what "the same every time" costs.
Our view, in short:
- Treat the spec sheet as a hint. The useful question is whether the process holds on your part, in your material, at the end of the run.
- Fix the setup before the machine. Locating features, tool setting and chip control solve more variation than any upgrade.
- Separate offset from scatter. One is a quick adjustment, the other is an investigation.
- Keep the machinist in the loop. Quick iteration only works when the person who sees the drift can act on it the same day.
We do not publish repeatability figures for our machines in this article, because a number without its test method would mislead you. What we can say is how we check: tool-setting checks, warm-up, first-article measurement and in-run sampling.
— Drake
When you need parts, not theory
If you have a prototype, a short run, or a fixture or bracket that needs to come out the same every time, we can help. We offer prototype machining, short-run production, and fixtures, brackets and support parts, with direct access to the machinist for quick iteration. Send the drawing and tell us which features are critical, and we will talk through what is realistic.
If you ride an electric mini, our E2 Kickstand is a bolt-on, CNC-machined alternative to the factory triangle stand for the KTM SX-E 2, GASGAS MC-E 2 and Husqvarna EE 2, priced at $100 to $105. If you are curious how a part like that gets made, our guide to machining motorcycle parts is a good place to start.
FAQ
What is the difference between repeatability and accuracy?
Accuracy is how close a result is to the commanded or true value. Repeatability is how closely the same motion or result can be duplicated. A machine can be repeatable but offset, or accurate on average but inconsistent from cycle to cycle, and the fixes differ.
Are precision and reproducibility the same thing?
Not quite. Precision is a broad term for how tightly results cluster, and repeatability is its tightest form, with operator, equipment and method held constant over a short time. Reproducibility changes those conditions, such as the operator, machine, fixture or day. In a shop, it means whether a different setup gives the same part.
What are the five axes of a CNC machine?
A 5-axis machine conventionally has three linear axes, X, Y and Z, plus two rotary axes, usually labeled A, B or C depending on the axis they rotate around. Layouts vary between builders, so confirm the configuration in the machine's documentation. The standard ISO 230-2 applies to both linear and rotary axes when testing positioning.
What is the repeatability of a robot?
There is no single value. It depends on the robot, its location in the workspace, end-effector mass, motion type, calibration, measurement method and environment. NIST notes that ISO 9283 provides standardized tests but that application-specific assessment is often needed. In one NIST example, a robotic drilling platform cut average hole error from 1.9 mm to 0.47 mm after tracker-based correction, which is an application result, not a general spec.
How can I check repeatability in my own shop?
Start with the tool-setting test: measure tool length 10 times with the manufacturer's cycle and calculate the range. Then measure a first article and a short sample of parts on a gage with enough resolution, and look at the spread separately from the average. Document the method so the next check is comparable.
Sources
- ISO 230-2:2014, accuracy and repeatability of positioning of numerically controlled axes
- Understanding CNC Machine Accuracy and Repeatability, Modern Machine Shop
- Precision in machining: research challenges, NIST
- On-Machine Measurement Use Cases and Information for Machining Operations, NIST
- Evaluation of on-machine probing test methods, NIST
- Traceability of On-Machine Tool Measurement: A Review
- In-process optical measurement and compensation of machine tool thermal deformations, NIST
- Vision-based thermal drift monitoring method for machine tools, NIST
- Milling stability study, NIST
- Terms used in metrology, NCBI Bookshelf
- Robotic drilling presentation, NIST (2025)